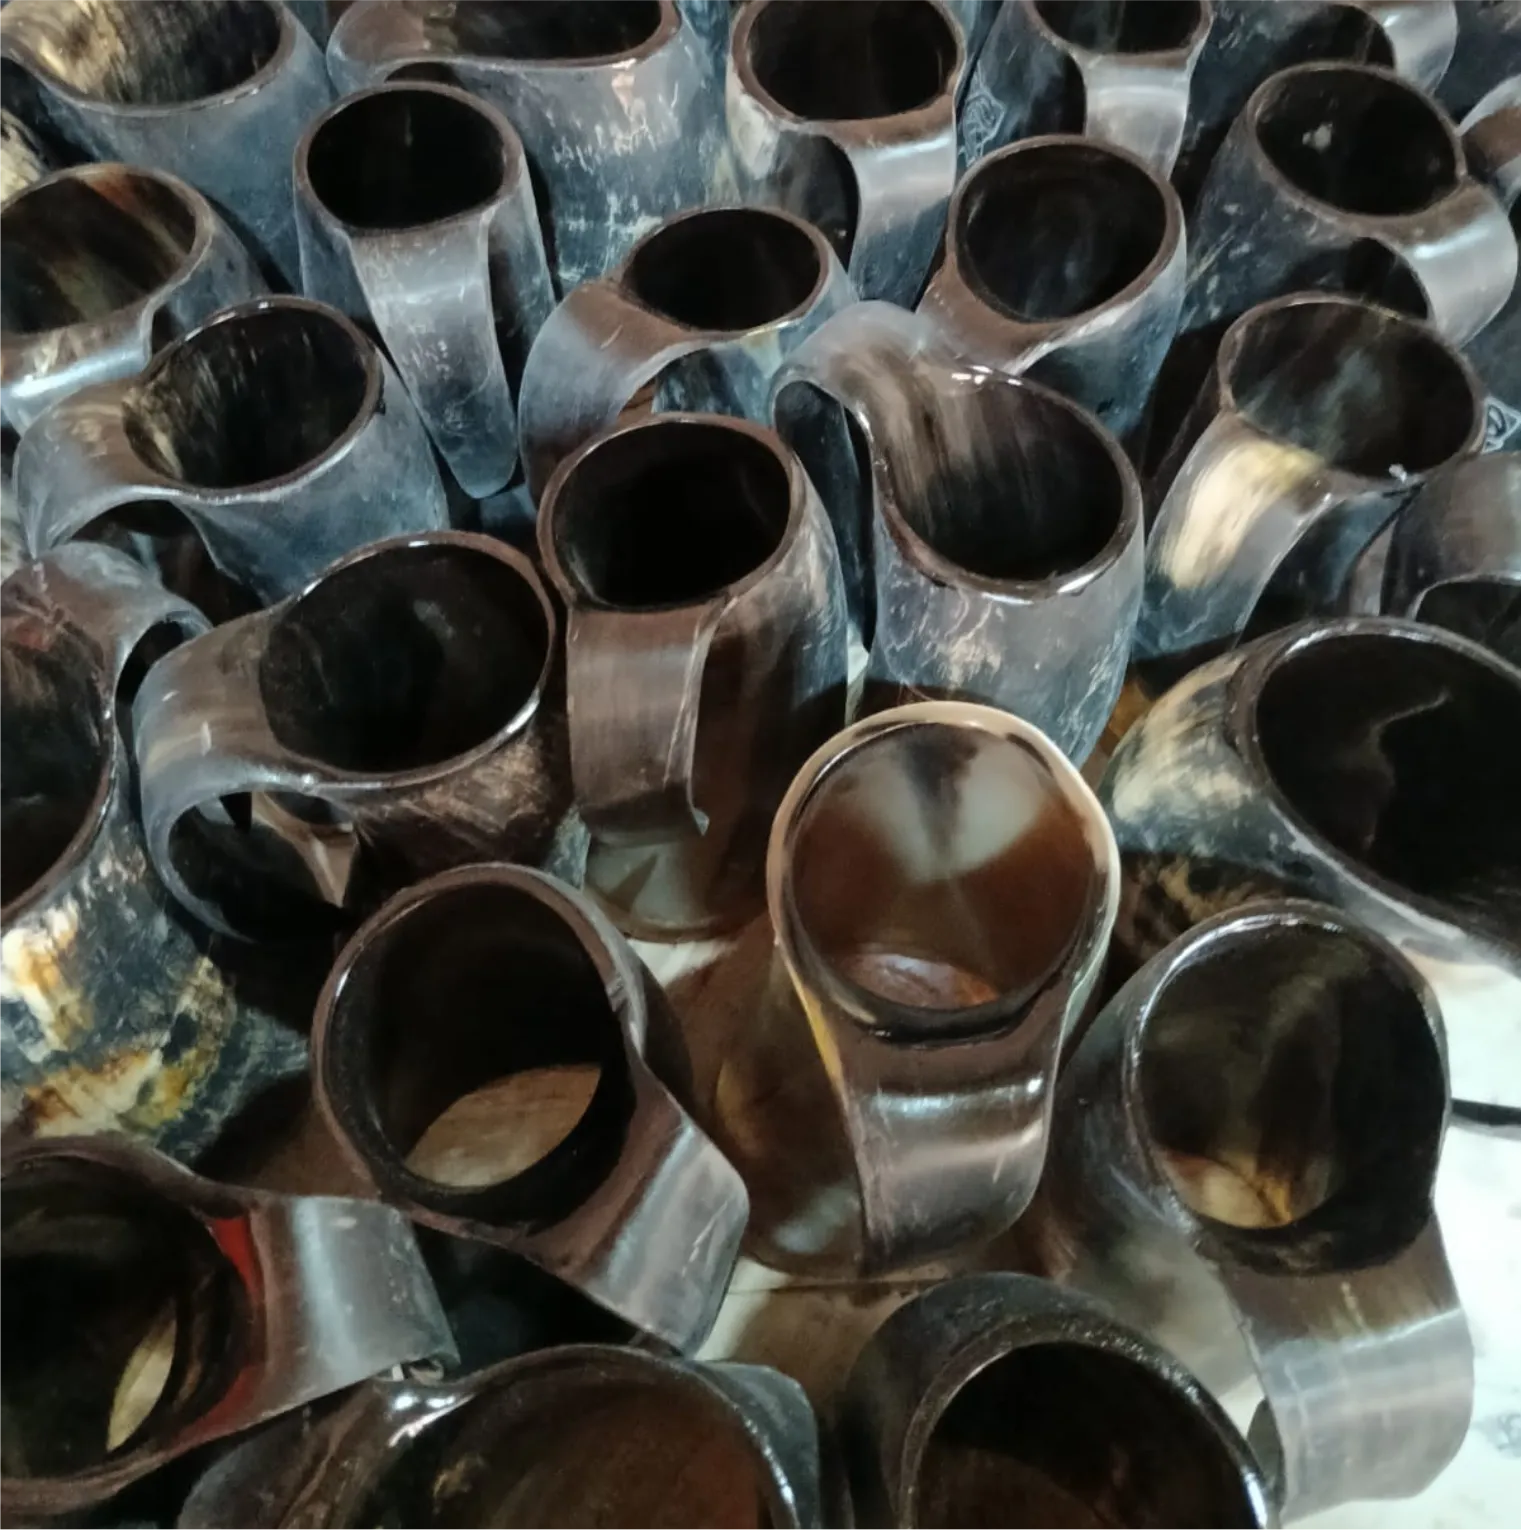
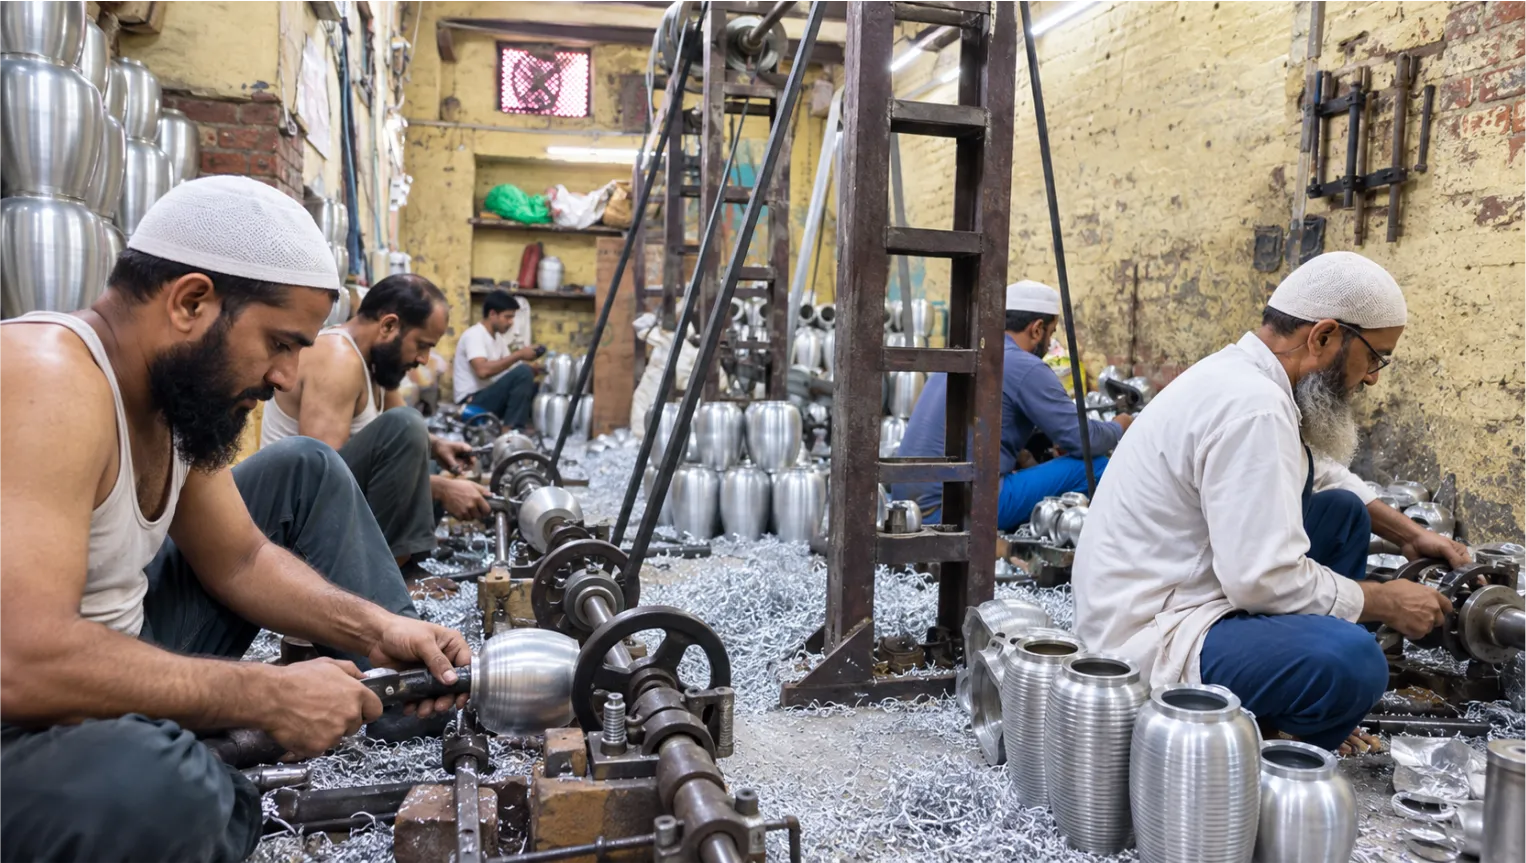
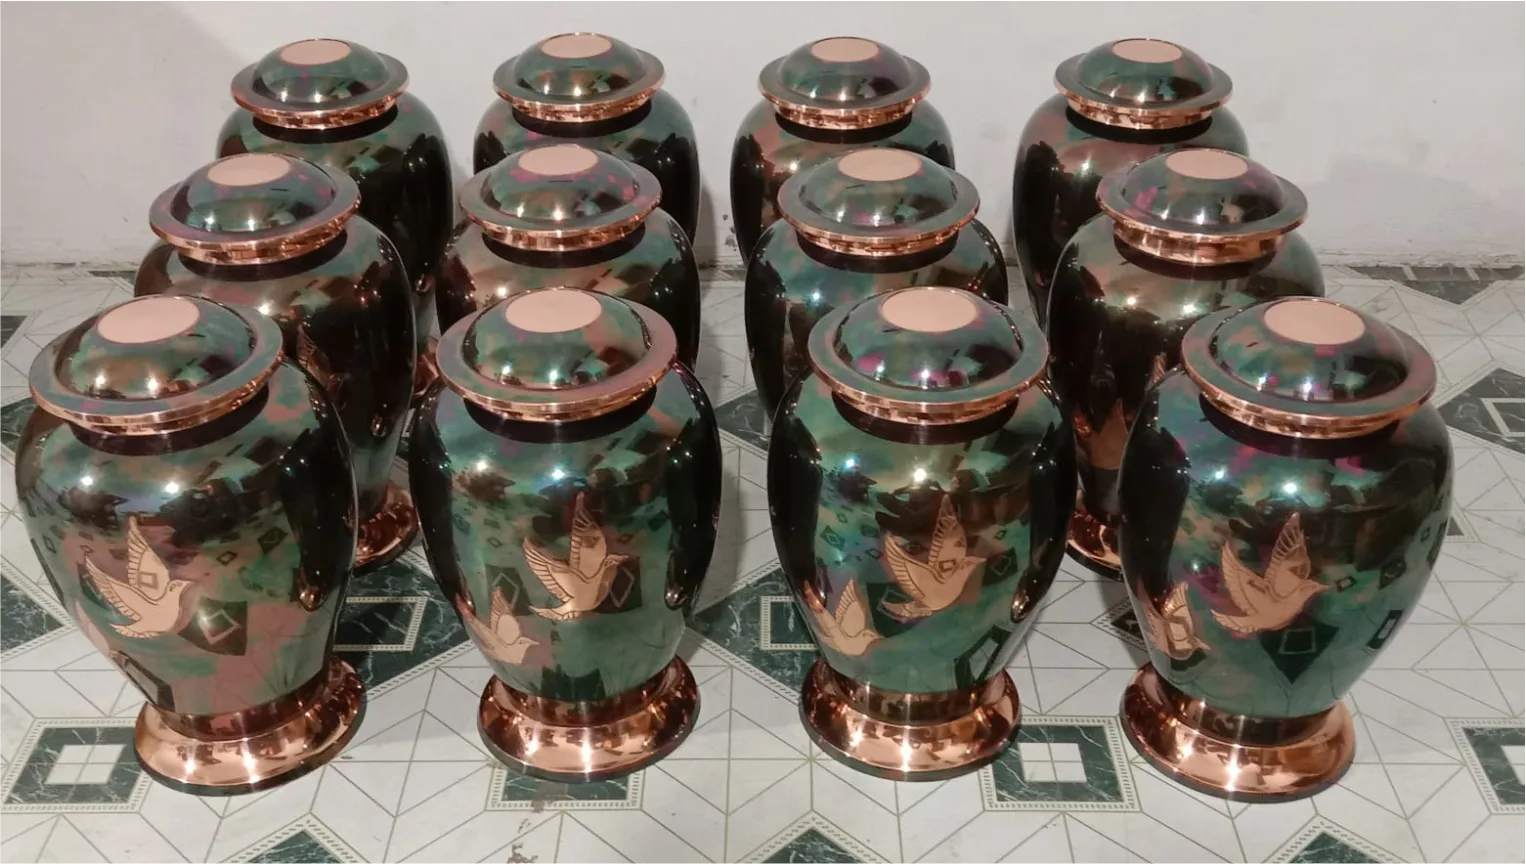
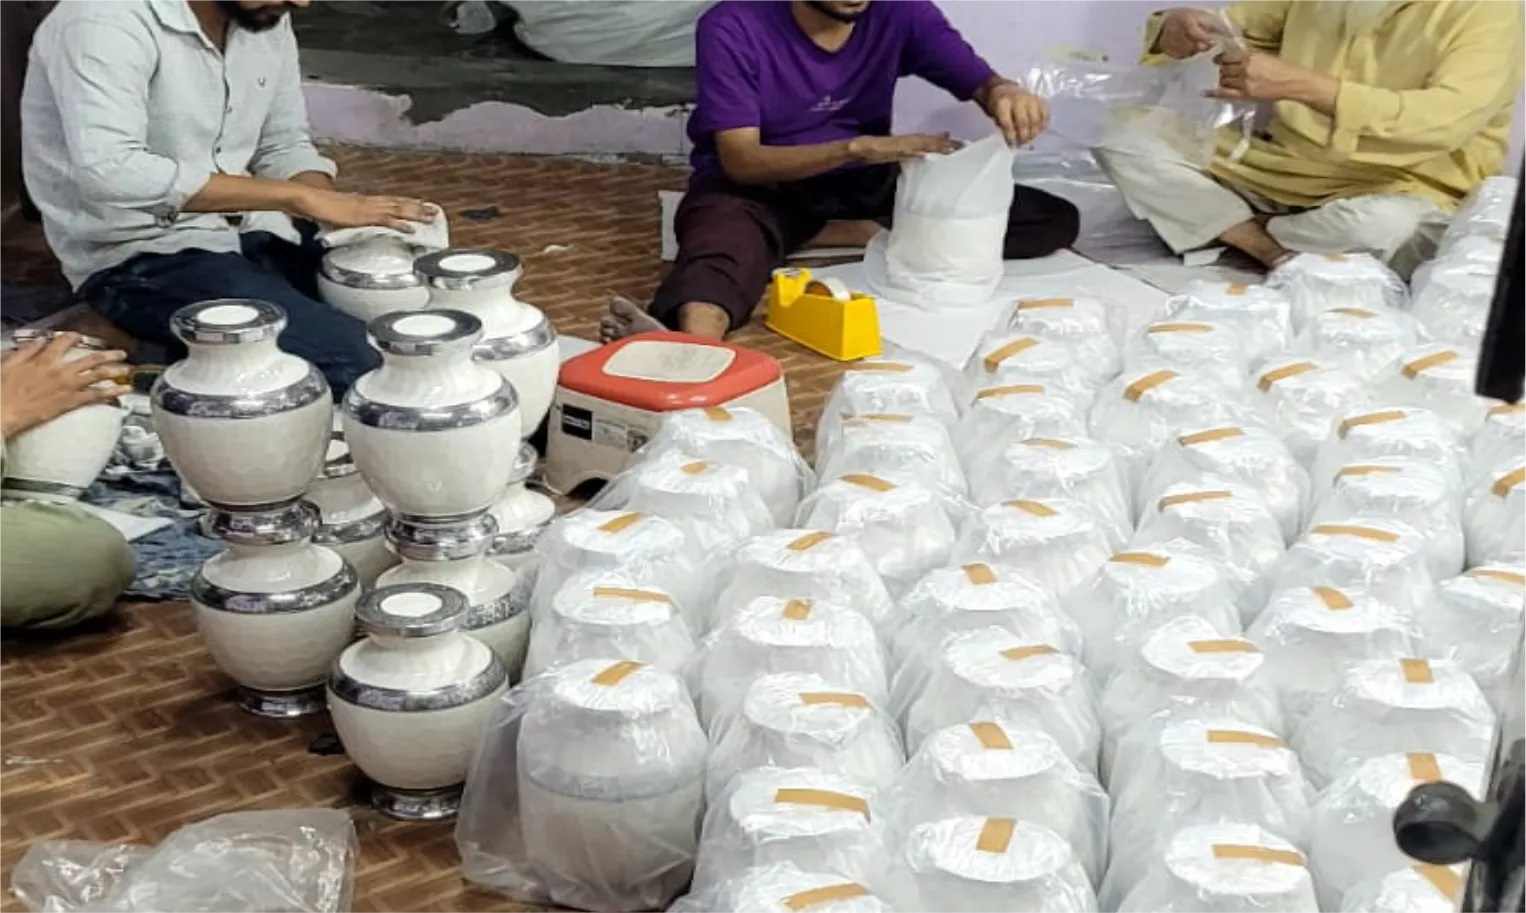
Our 4,800 sq. ft. manufacturing facility is divided into seven dedicated departments, each arranged around a specific stage of production. This structure helps us maintain better control over material movement, workmanship, inspection, finishing, packing, and dispatch. Every department has defined equipment, operating responsibilities, and practical production limits so buyers can understand exactly what is handled within our facility.
We prefer to be clear about our actual manufacturing capabilities rather than present outsourced processes as in-house operations. The facility audit covers available floor space, key machinery, workforce allocation, monthly production capacity, quality-control checkpoints, and any specialised work completed through approved external vendors.
Our 4,800 sq. ft. manufacturing facility is divided into seven dedicated departments, each arranged around a specific stage of production. This structure helps us maintain better control over material movement.
Material moves one way, raw store to packing, no doubling back, while equipment on the floor honestly matches the claimed capacity.
| Department | What Happens Here |
|---|---|
| Raw material store | Incoming horn and timber received, graded and stacked by size and quality band. Rejected stock is separated before it enters production. |
| Cutting & horn pressing | Horn sectioned, heated and pressed to the ordered curve or straightened for tankards. Timber cut to blank size. |
| Turning & grinding | Lathe work on wood and horn. Capacity ground to spec, wall thickness taken down, interiors bored. |
| Metal spinning | Brass and aluminium urn bodies spun and trimmed. Rims, stand rings and metal edging formed. |
| Leather section | Veg-tanned hide cut, punched, dyed and stitched for holsters, belts and carry straps. |
| Finishing & engraving | Sanding through grits, buffing, lining and sealing. Laser and hand engraving applied last so artwork is never lost to a later process. |
| QC & packing | Leak testing, gauging, weighing, labelling and carton packing against the buyer's packing list. |
| Equipment | Used For |
|---|---|
| Wood turning lathes | Mugs, tankards, yarn bowls, crochet hooks, urn bodies, stand components |
| Horn pressing / heating setup | Straightening and curving raw horn to the ordered profile |
| Bandsaw & cutting | Sectioning horn, cutting timber blanks |
| Grinding & sanding stations | Wall thickness reduction, capacity grinding, grit progression |
| Buffing / polishing mops | Final horn and wood polish |
| Metal spinning lathe | Brass and aluminium urn bodies, rims, rings |
| Laser engraver | Logos, names, runes and artwork on horn, wood and metal |
| Drilling & boring | Stand fittings, holster rivets, urn threading |
| Leather stitching & punching | Holsters, belts, straps |
| Weighing & gauging tools | Capacity check, wall gauge, batch weight |
The amount of work in our factory is determined by the complexity of the item, materials and hand-finishing needs. Instead of reporting one generalized number of production, we divide our daily throughput into different product categories, giving you a precise idea of our real manufacturing capacity and lead times.
Designed to maximize high-throughput pressing, curving and wall-thickness grinding of natural drinking horns, tankards and custom hand-engraved work.
Specific high-precision wood, brass and aluminum urn assembly dedicated to turning, metal spinning and lacquering arrangements.
Scalable floor space to do the precise wood turning, hook shaping and smooth buffing of yarn bowls, crochet hooks and decor.
Cutting, vegetable dyeing and sewing department to do custom holsters, carry straps, and final protective surface finishes.
| Range | Monthly Output | Slowest Stage | Typical Lead Time |
|---|---|---|---|
| Cremation urns — wood | 400 | Turning and oil finishing | 25–30 days |
| Cremation urns — brass / aluminium | 600 | Spinning and lacquering | 30–35 days |
| Drinking horns — natural | 500 | Pressing and interior sealing | 25–30 days |
| Drinking horns — engraved / personalised | 400 | Engraving and artwork proofing | 30–35 days |
| Horn mugs & tankards | 300 | Wall grinding to capacity | 25–30 days |
| Blowing horns | 400 | Bore tuning and strap stitching | 25–30 days |
| Wooden décor & ship wheels | 500 | Assembly of spokes and rim | 25–30 days |
| Crochet hooks, yarn bowls & winders | 1200 | Hook shaping and sanding | 20–25 days |
We have distinct operational lines in all our lines of products. The following is the actual work breakdown structure of the core urn-making processes and secondary craft lines which will be dealt with on our factory floor.
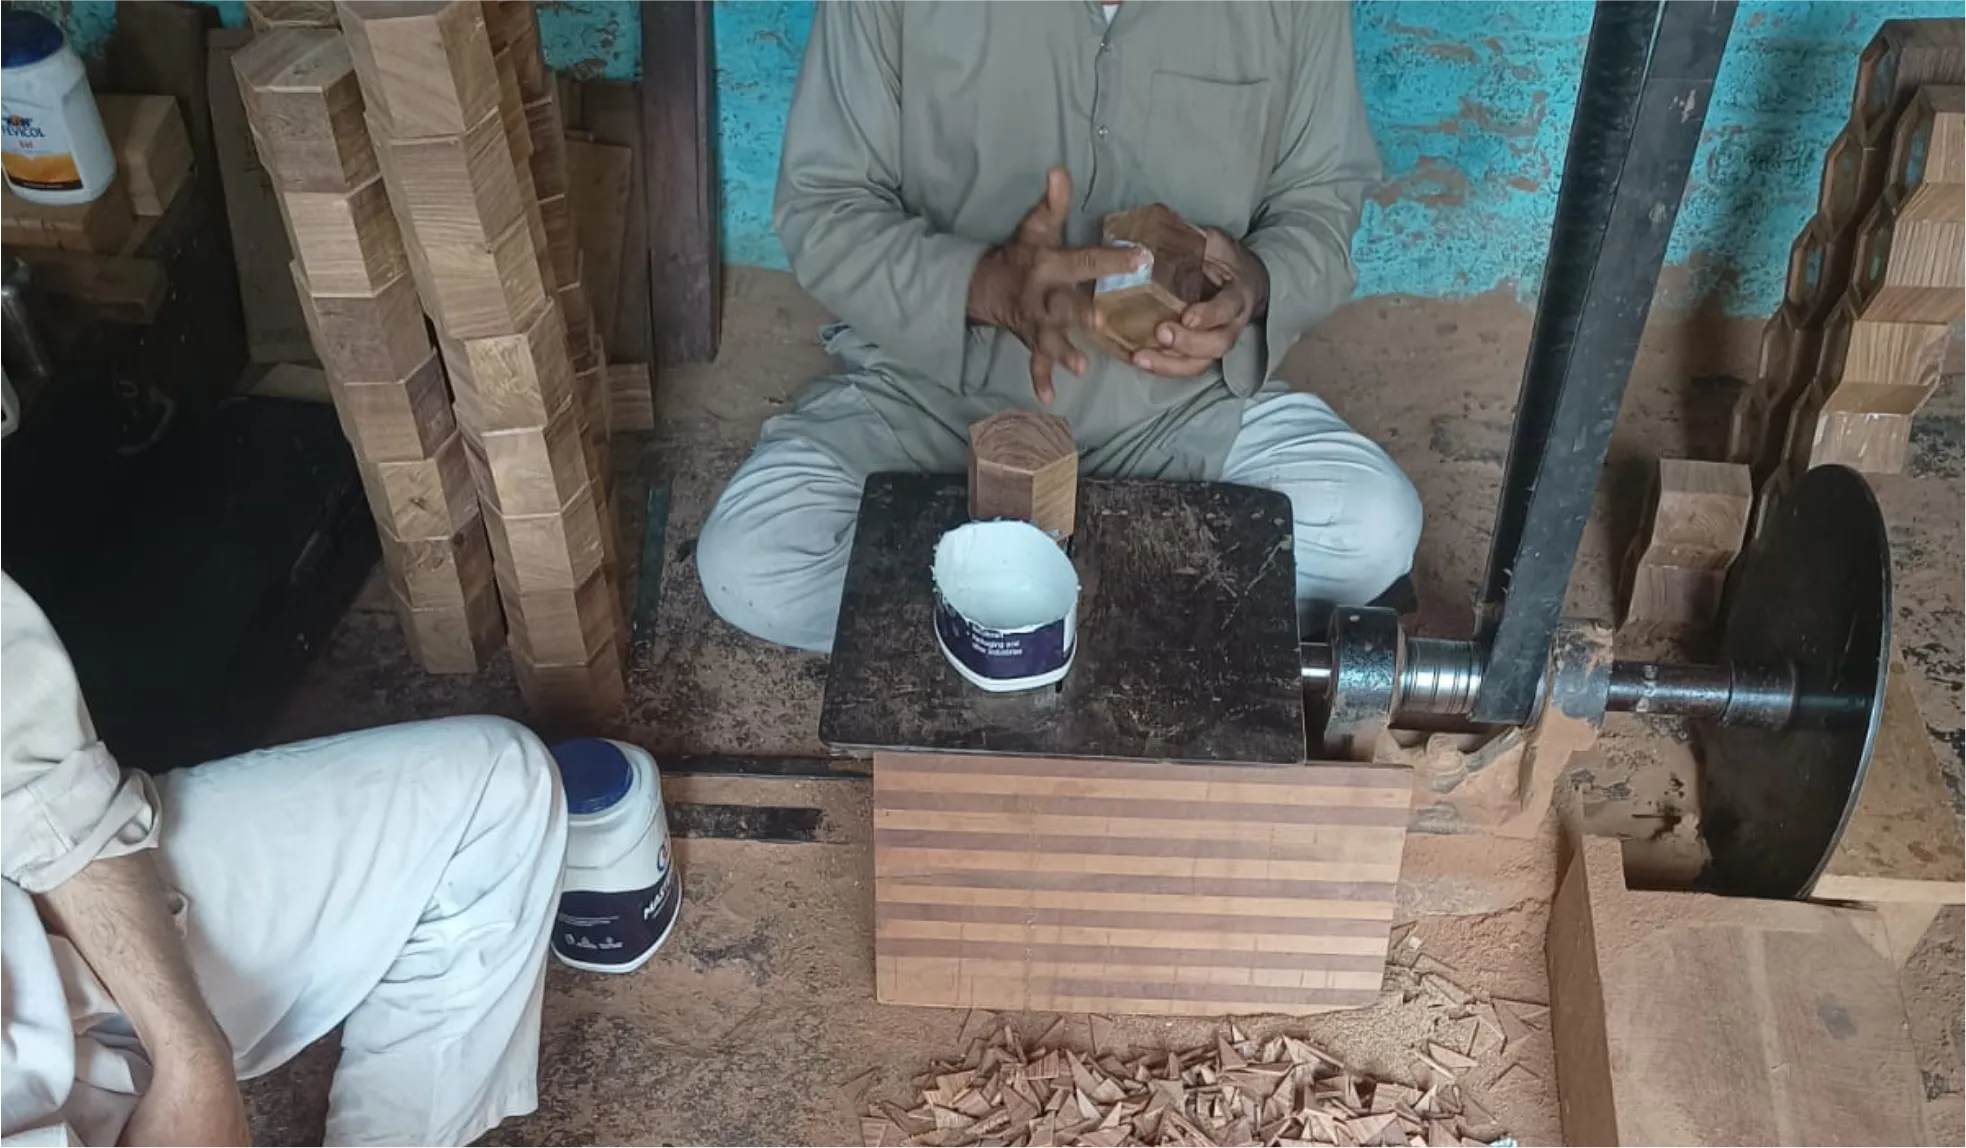
Any working day, on WhatsApp video, we will walk the floor in the order material moves through it. No appointment and no notice needed.